Sunday, 17 March 2024

"Can you smile with DIAMONDS IN YOUR TEETH?" - 26 photos (of diamond studded teeth)

 I looked into my archives and found that some very important photos were missing. Here are the extra 'smiling' photos that needed to be displayed again, in greater 'text' detail. 


 I selected a series of very large diamonds, these will be placed in the center of each tooth, why is this? I want the eye to gravitate to the center of each tooth and the smaller stones to be 'little extra bursts of light'.
 Every center stone will have '8 beads' holding each stone.
Excessive polishing on the setting areas is not required, as this is where the multitude of diamonds will be situated.


 My client gave me 'mediocre quality' and the colour of diamonds were also lacking. My job was just to bead set those diamonds and 'enjoy the ride'.
 If I 'find' a pin-hole from the casting, that is where some of the diamonds will be set.

 I like to keep my tool selection to a minimum, why is this? If I drop a stone, I won't have to keep looking for it around my other unused setting tools.

 These are my assortment of burs, I like to keep my burs in an orderly layout.

 This is my Onglette #2, Bead-Raiser that will be used to set these Diamonds. There are well over 600 diamonds in this 'set of teeth'.
 This Beading-tool that I used is an Onglette graver of #2 that is measured in it's width. To avoid the tip of the graver from breaking, I 'round' off the tip of this tool.
 
 All over each tooth, there will be many diamonds. I estimated that there are 16-18 stones PER TOOTH.

 There is little opportunity in doing any Bright-Cutting, my client wanted only "Diamonds and Beads" to be seen on each tooth.

 There is little space to do any graver-cutting, that is because of the close proximity to all of the stones.

 Once that a group of stones are set into each tooth, I will start the 'beading process' around the center stone. Even the layout of beads is so very important, as the beads will be located in between each stone (as shown).

 You can see the overall layout of each Bead to the center diamond. That Bead MUST BE POSITIONED OVER THE GIRDLE OF THE STONE. 

  Every few minutes, I will apply my Onglette to a 'semi-rough' Emery Paper of #400 grit.
 I don't want any bead to get ruined by having the graver to 'slip & slide' along the metal.
 
 The graver must be rubbed along the paper, this rubbing is done under and against the underneath section of the blade. I'm giving a "texturing" effect to the blade.

I'm using my mini-torch to adjust the positioning of the few teeth to my Shellac-Stick.

 I want to have the shellac get very soft (almost watery) as I need to have the 'underneath' give support to the few teeth. 
Even on this photograph, I will 'move' the teeth just a bit further, how much? I need and want the tooth to be in the center of my 'stone-setting' position on the shellac stick.

 
 For further underneath support, I will rest the tooth against and on my bench-peg. 

The 'beads' as shown, must be literally 'against and over' the Girdle of every stone. Use your 10x power Loupe and examine each bead for this rule.


Many times these sets of teeth are not made in thick gold, this is because of the weight problem on the persons jaws and its many teeth.
 I suggest not to drill a large hole into the metal. You need the 'angled metal' to allow the diamond to be resting against this metal. 

 I always sift through the many hundreds of diamonds and put them into groups of sizes and stone-colours.

 After the first stone is set, it's always better to study the layout for the first group of stones. From here the minor indentation is ready for drilling of the holes, BUT NOT ALL OF THEM AT ONCE. 

  You can now see where all of the beads have now been created? Even if there are spaces in between any stones, just raise "decorative beads" in between those stones just to fill in any gaps.

 I wanted to do some testing if any Onglette cutting would be required, I did only one line on each tooth. (I wasn't too pleased with these results) PITY!

These 'temporary' and as well partially drilled holes served only as a guide for the actual hole spacings. If I was satisfied, then I completed the drilling processes for each tooth.

 For each 'temporary hole' I completed the drilling with my thin twist-drill. But NEVER FOR THE SIZE OF THE STONE. I needed the balance of the 'curved hole surface' just to allow the Pavilion of the stone to sit against it.


NOW YOU CAN SMILE WITH THESE (Diamond Studded) TEETH.

Friday, 15 March 2024

"Fish-Tail" design with Bright-Cutting & "156C" bur - 29 photos

 "Fish-Tail" gemstone setting is one of the most intricate designs that can be created without any CAD (computer aided design) program. 
 I'd rate this exercise at about "18+ out of 10". The only tools that I use are a Flat graver of #40 width that is used for Bright-Cutting (for a much required wider cut).
(This essay was originally dated Nov. 2023, I feel that it's necessary to review this again, but with many greater photo details.)

 WHY IS THIS NAMED "FISH-TAIL"? The two beads are the fish's eyes and the two curves are it's tail-fins.
=============================================


One of the many designs I use extensively is using solely a Flat graver #40 in width. To initiate the cutting, I start with the corner of the blade as being shown here.
 In one single cut, the whole blade comes into full use.

 I didn't (on purpose) burnish the 'beads'. I was more interested in getting the stones set that I had more things to do. For example Bright-Cutting the metal.....everywhere!

 My emphasis during this stage of metal-carving is to make sure that the beads are now 'rounded'.

How do I keep the stones in the 'fish-tail' design? This is so very easy, let's start to explain this interesting technique.
 I will carefully grab the Fish's curved areas and pull the curved areas together with a pair of fine-toothed jaws. If you wish to use your 'hand-pusher' that is another option.

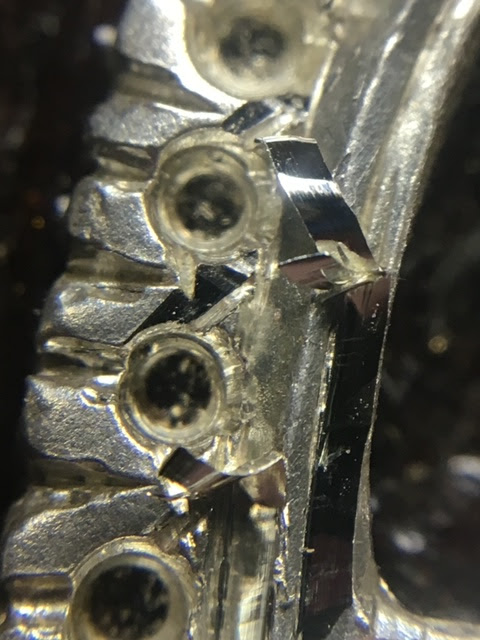
 On either side of the 'fish's tail' are these two seats. I will use my 156C (Carbide) bur and create two seats inside of the hole, this where the gemstone will sit, but not securely!!!

You can easily see the '156C' under-cutting bur making a seat inside the hole. This 'bearing-carving' must be formed all around the hole, as this is where the stone will sit.

      In this up-close photo shows the bur in action.

Long before any gemstone is set, much care is taken in cleaning all of the areas that is to shine from the "Bright-Cutting" processes.


This great photo is showing you some of the bearings where the stone will sit. With your bud-shaped bur cut at an angle in between the two beads. 
THERE MUST NOT BE ANY EXTRA METAL remaining in between the two beads. Get it removed NOW!


Don't be too cautious in using your 156C bur. Utilize the edges of the 'rotating bur' to navigate around the hole. From here you will have a nice seat for every stone.

"Bright-Cutting" is the most challenging aspect of this pattern. You are not removing or destroying any areas of the design, but enhancing the pattern many times better.
 The enhancing makes every metal angle 'bright and shiny'.

This sliver of metal is from the Flat graver doing what it's supposed to do. It's to give lustre to the 'rough-cutting', there must not be any lines in the face of the graver.
 If the graver face is poorly polished (on your polishing paper & oilstone) then those 'graver defects' will leave poorly created lines in the fish-tail pattern.
KEEP YOUR TOOLS CLEAN AT ALL TIMES.


This photo displays the bright cutting edges that we are all aiming for, agree?
 
 To review again, use your #004 bud-shaped bur and keep the metal clean of any extra metal in between those two beads. All that you should have are two little 'posts'. These two posts are your new beads.


Your Flat graver is again 'doing it's magic' on the metal. Keep your tools sharp!!!


        'Bud-Shaped' bur can do so much in this subtle metal carving.


The Bright-Cutting results shown in this photo, are only 'mediocre' but not very clean.

In this better photo, you can see how important a pristine looking Flat graver can be.

 With a Flat graver, every section of the front of the blade is doing wonderful things to the metal. By starting at the edge and slowly working with the center of the blade, every millimeter of the Flat graver is being used.

This is my epitome of a good polishing paper, I use any polishing paper from #800 grit all the way up to a #1,200 grit, why? I WANT PERFECTION, nothing else!

 My burs come in various sizes and shapes, eventually every bur will be used.

 I will place this setting process at "18 out of 10". But once that these techniques have been learned, then come the practising, this practising "Fish-Tail" took me 2 YEARS.